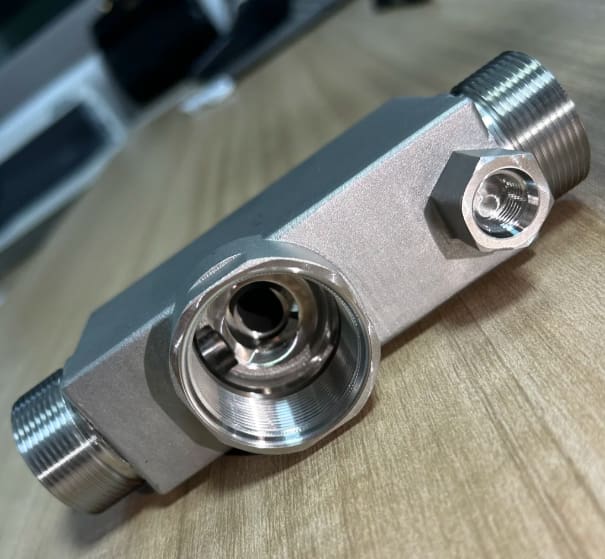
In the world of fluid dynamics and industrial plumbing, a component is only as good as its weakest connection. For procurement managers and engineers sourcing critical fluid control parts, the “simple” manifold is rarely simple. It represents a complex intersection of metallurgy, thermal dynamics, and subtractive manufacturing.
Today, I want to break down a specific project—a custom stainless steel manifold—to explain how we maintain tight tolerances even after introducing the extreme heat of fabrication.
Table of Contents
- The Engineering Challenge: Fabrication vs. Precision
- Visual Analysis: Deconstructing the Manifold
- Controlling the HAZ: Welding Without Warping
- Surface Finish: More Than Just Aesthetics
The Engineering Challenge: Fabrication vs. Precision
The fundamental conflict in manufacturing fluid components is that CNC machining services rely on rigid stability to achieve tolerances of ±0.01mm, while welding introduces massive thermal expansion and contraction.
When you weld a port onto a turned tube, the metal pulls. If that tube has already been threaded, the heat can ovalize the thread profile, turning a Class 2A fit into a scrap part that leaks under pressure. The component shown in the image above is a textbook example of how to execute this process correctly. It requires a strict order of operations:
- Rough Turning: Establishing the main geometry.
- Precision Fabrication: Welding ports with heat sinks.
- Finish Machining: Cutting final threads and sealing faces after the stress has been relieved.
Visual Analysis: Deconstructing the Manifold
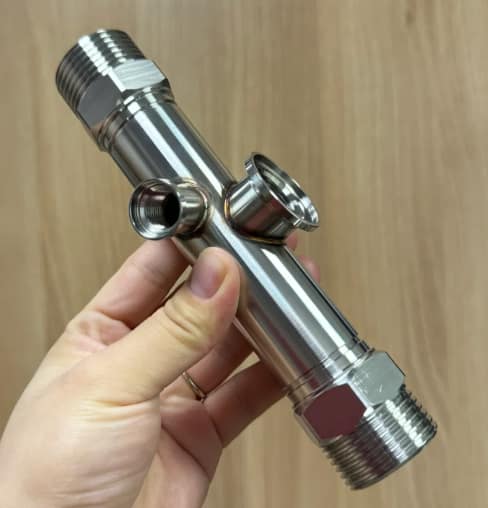
Let’s look closely at the part I’m holding in the image. This isn’t off-the-shelf hardware; it is a bespoke solution likely designed for a high-purity fluid or gas application.
- Material: The luster and grain suggest Stainless Steel 316L. This grade is preferred for its superior corrosion resistance and lower carbon content, which prevents carbide precipitation during welding.
- The Main Body: The central tube features CNC turned ends with male threads (likely NPT or BSPT). Notice the machined hex flats. These were milled directly into the round stock or turned from hex stock to allow for wrench tightening during assembly without damaging the cylindrical body.
- The Junctions: There are two distinct ports added via fabrication.
- Port A (Left): A smaller threaded boss, likely for a sensor or gauge.
- Port B (Right): A flanged fitting, possibly a sanitary ferrule connection.
- The Weld Quality: The “rainbow” coloration around the joints is the Heat Affected Zone (HAZ). In this state, the oxidation colors indicate the temperature reached. The tight, consistent bead suggests Manual TIG (GTAW) by a skilled operator, ensuring full penetration without burning through to the ID (Inner Diameter).
Controlling the HAZ: Welding Without Warping
The most critical aspect of this part is the transition mentioned in the social post. How do we ensure the side ports are perpendicular to the main axis and the main threads remain concentric?
Furthermore, regarding the threads: notice how the threads near the hex flats are pristine. If we were to weld too close to a finished thread without protection, spatter or distortion would ruin the pitch diameter. The design here smartly places the welds at the mid-section, isolating the critical sealing surfaces from the highest heat input.
Surface Finish: More Than Just Aesthetics
In the image, the part has a semi-polished, machined finish. However, for industries like food processing, pharmaceuticals, or semiconductor manufacturing, the surface roughness (Ra) is a functional specification, not a cosmetic one.
Rough surfaces trap bacteria and create turbulence in fluid flow. The post mentions a “sanitary-grade polish.” To achieve this, we employ various surface finishing techniques:
- Electropolishing: This removes a microscopic layer of material, smoothing out peaks and valleys to improve corrosion resistance and reduce Ra to <0.4µm.
- Passivation: Using citric or nitric acid to remove free iron from the surface, enhancing the natural oxide layer that protects stainless steel.
The part in the photo shows a clean “as-machined” and “as-welded” state. For a final production run, we would likely pickle and passivate the weld seams to remove the heat tint and restore full corrosion resistance to the HAZ.
What Buyers Should Verify
Before placing an order, confirm material grade, tolerance-critical features, inspection methods, finishing limits, packaging, lead time, and applicable certifications with the selected manufacturing partner. SP Precision coordinates RFQ review, DFM communication, quotation, and supplier follow-up; project-specific production capabilities and certification documents are confirmed before order placement.