In the world of fluid power and subsea engineering, a component failure isn’t just an inconvenience—it’s a catastrophe. Whether you are designing for offshore oil rigs or heavy industrial hydraulics, the integrity of your connection points is non-negotiable.
Today, I want to walk you through a recent batch of heavy-duty stainless steel fittings we produced. We will analyze the specific machining challenges presented by this design and discuss why precision manufacturing is the only safety factor that truly matters.
Table of Contents
- Visual Analysis: Built for Hoop Stress
- The Material Challenge: Machining Stainless Steel
- Critical Features: Threads, Bores, and Finishes
- From Prototype to Production
Visual Analysis: Built for Hoop Stress
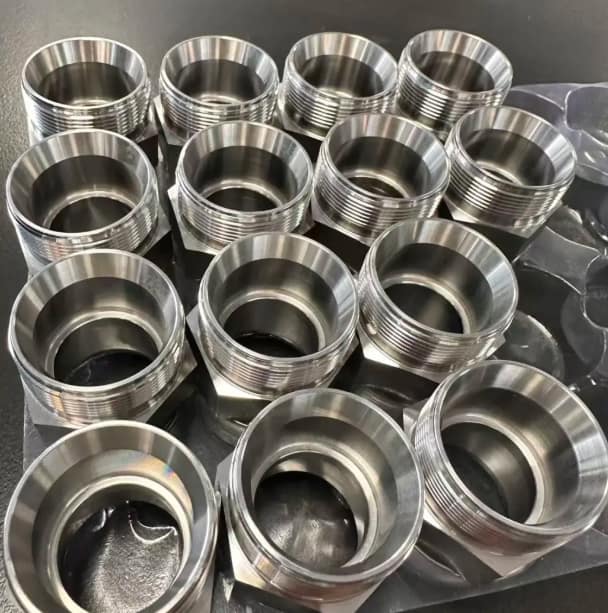
Take a close look at the image above. These aren’t your average hardware store plumbing parts. As a manufacturing specialist, several features immediately stand out to me regarding the design intent and the machining strategy required.
The most obvious feature is the wall thickness. In hydraulic applications, hoop stress (the force exerted circumferentially perpendicular to the axis and the radius of the cylinder wall) is the primary enemy. The designers here prioritized a massive safety factor.
From a manufacturing standpoint, this part features a hexagonal base transitioning into a cylindrical threaded section. This geometry suggests the raw material was likely high-grade hexagonal bar stock, processed on a CNC turning center. The substantial mass of the part aids in vibration dampening during the cutting process, but it also requires rigid workholding to prevent chatter when turning those critical external threads.
The Material Challenge: Machining Stainless Steel
Based on the application profile—high-pressure hydraulics or subsea environments—these parts are almost certainly machined from Stainless Steel 316 or 316L. While 304 is common, 316 offers the molybdenum content necessary to resist pitting in chloride environments (like seawater).
However, stainless steel is notorious for work hardening. If your CNC machining services provider uses incorrect feed rates or dull tooling, the material hardens instantly at the cutting interface. This leads to:
- Premature tool failure.
- Poor dimensional tolerances.
- Induced internal stresses in the part.
Critical Features: Threads, Bores, and Finishes
The “devil is in the details,” as the saying goes. In high-stakes manufacturing, the details are defined by GD&T (Geometric Dimensioning and Tolerancing). Let’s break down the three critical areas of these fittings.
1. The Internal Surface Finish
Looking down the bore of these fittings, you will notice a distinct lack of tool marks. In hydraulic systems, fluid turbulence causes heat and efficiency loss. A rough internal bore can also become a nucleation site for corrosion or fatigue cracks.
We target a specific Ra (Roughness Average) value—typically Ra 0.8µm or better for these applications. Achieving this requires a final finishing pass with a specialized boring bar or a honing process. For applications requiring mirror-like smoothness, we can also apply advanced surface finishing techniques such as electropolishing, which not only smooths the surface but enhances the passive oxide layer of the stainless steel.
2. External Threads and Galling Prevention
The external threads shown in the image are cut cleanly with no burrs. In stainless steel applications, galling (cold welding) is a significant risk during assembly. If the thread quality is poor or the pitch diameter is slightly off, the friction during tightening will cause the male and female threads to seize together permanently.
We prevent this through:
- Single-point threading: Using CNC turning for precise thread profiles rather than using a die.
- Thread Gaging: Every batch is checked with Go/No-Go gauges to ensure compliance with UN or Metric standards.
3. Chamfers and Handling
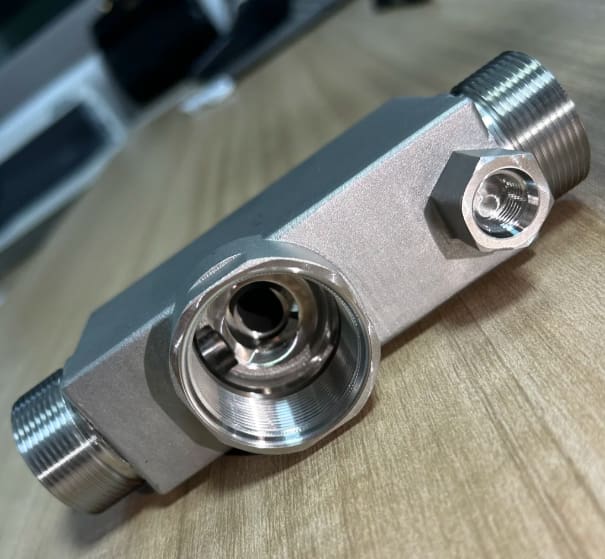
You will notice generous chamfers on the hex edges and the thread lead-in. While this aids in assembly, it is also a safety feature for the assembly technicians. Burrs on stainless steel are razor-sharp. A proper chamfer ensures the part can be handled safely despite its heavy weight.
From Prototype to Production
When developing components for high-pressure systems, you rarely go straight to mass production. You need to validate the design first.
Perhaps you need to test different wall thicknesses to balance weight vs. burst pressure, or maybe you need to test 316L versus 17-4 PH stainless steel. This is where rapid prototyping becomes essential.
What Buyers Should Verify
Before placing an order, confirm material grade, tolerance-critical features, inspection methods, finishing limits, packaging, lead time, and applicable certifications with the selected manufacturing partner. SP Precision coordinates RFQ review, DFM communication, quotation, and supplier follow-up; project-specific production capabilities and certification documents are confirmed before order placement.
Ready to secure your supply chain?
If you have a design that requires heavy-duty turning, tight tolerances, and materials that are tough to machine, let’s talk. Whether it’s for hydraulic, aerospace, or industrial applications, we have the capacity to handle the pressure.